In advanced prototyping, tolerances define the line between a flawless charm and rework. This guide dives into tolerance ranges for 316L stainless steel charms and how finishing choices like PVD coating and electroplating influence geometry, fit, and performance across markets. For product developers, a disciplined approach to tolerance reduces lead times and ensures consistent plating quality across batches. This is essential for private-label programs and wholesale partnerships requiring repeatable quality under SGS-certified processes.
Stainless Steel Charm Tolerance Range for Prototyping
Understanding basic tolerances
Tolerance is the permissible variation from nominal geometry. For 316L stainless steel charms, typical linear tolerances for small features (holes, slots, holes through walls) range from ±0.05 mm to ±0.20 mm depending on feature size and process. Overall form tolerance accounts for machining, joining, and finishing steps, including polishing and plating. It’s common to budget a separate plating tolerance when finishing is applied after primary manufacturing.
Dimensional tolerance by feature type
Outer profiles, holes, and through features each carry different tolerance budgets. Small features like pin holes or through-holes may tolerate ±0.05–0.15 mm, while larger exterior profiles may be ±0.10–0.20 mm. Feature-to-feature stack-ups should be assessed early, especially when multiple operations occur between the blank, primary machining, and finishing stages. When parts require hole alignment to a mating component or jump rings, tolerance alignment is critical to avoid binding or misfit during assembly.
Finishing and its Impact on Tolerances
Finishing steps such as PVD coating, electroplating, enamel color filling, and crystal inlay add thickness and can shift critical dimensions. PVD coating thickness is typically measured in microns (0.5–5 μm common for jewelry-grade finishes), while electroplating can add roughly 0.5–2 μm. Enamel fills and crystal inlays add depth and may alter perceived tolerances when fills sit above recessed features. Designers should allocate a plating allowance and specify uniformity targets (thickness variation across the charm) to minimize dimensional drift between runs. Our capabilities in PVD plating and enamel filling support tight, repeatable finishes while maintaining geometry across batches.
Measurement and Verification Methods
Accurate verification relies on calibrated tools and documented procedures. Use calipers and micrometers for basic checks, and employ optical measurement or 3D scanning for complex contours. A coordinate measuring machine (CMM) or high-precision optical profiler helps quantify flatness, hole diameters, and edge radii with traceable references. Establish a measurement plan that covers nominal geometry, critical features, and finishing-induced bias to ensure consistent results from first article through production.
Process Controls for Consistency
Consistency comes from controlled jigs, fixtures, and process windows. Set machining offsets, preset tool wear allowances, and standardized polishing sequences to limit variance. Maintain a robust plating protocol with documented current, temperature, and immersion times for both PVD and electroplating stages. For cross-market programs, implement a uniform quality protocol that aligns with SGS certifications (RoHS, REACH, Nickel Release EN1811, Salt Spray 240H) to support global compliance and supplier confidence. OEM/ODM manufacturing capabilities and sample development programs help translate tolerances into repeatable production, especially for private-label packaging and wholesale distribution.
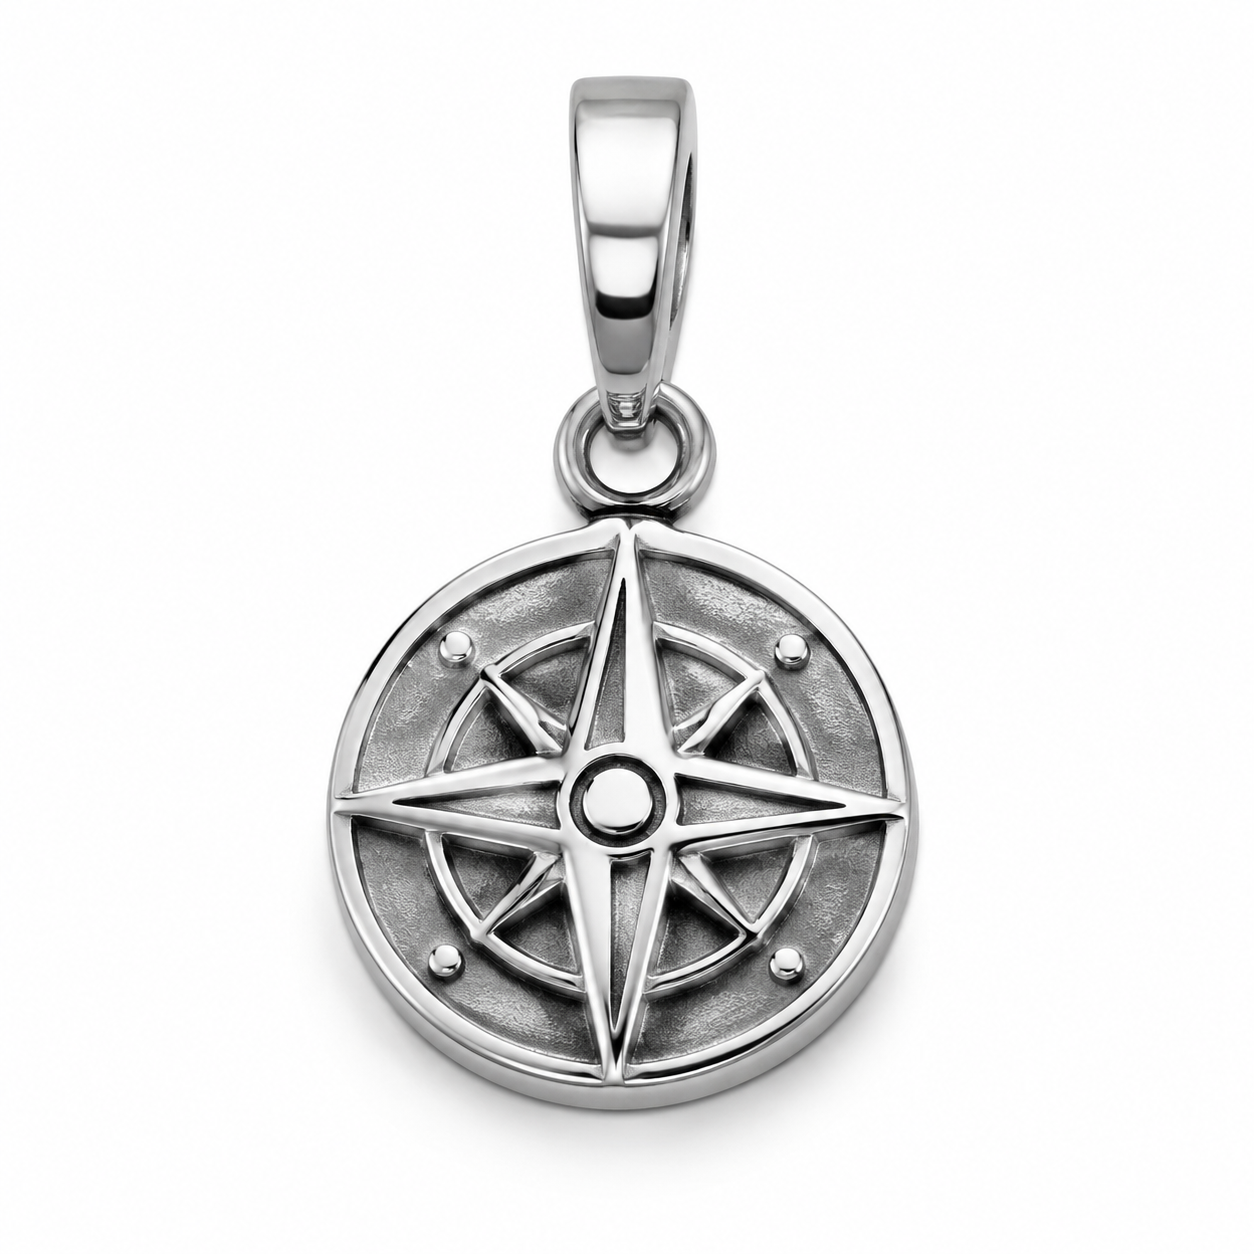
Why tolerances matter for finishing and market readiness
Key benefits
- Consistent plating quality across runs and batches, reducing rework.
- Predictable fit with mating components, jump rings, and clasps, improving assembly yield.
- Better alignment with private-label packaging and boutique programs, enabling reliable MOQ adherence.
- SGS-certified processes support regulatory and retailer expectations for RoHS, REACH, Nickel Release, and corrosion tests.
- Faster sample development and iteration cycles for OEM/ODM collaborations, with clear dimensional budgets.
Detailed analysis and step-by-step guide
Step 1: Define functional requirements and geometry
Begin with a precise nominal geometry and a clear list of critical features (hole diameters, outer profile, radii, and thickness of plating). Identify which dimensions impact assembly and visual tolerance, and decide which features are “hard” (tight tolerance) versus “soft” (slightly forgiving). For public or private-label programs, document the nominal size in a drawing pack and align expectations with the OEM/ODM partner to ensure the tolerance plan supports the intended finish.
Step 2: Plan tolerance stack-up and feature budgets
Construct a tolerance stack-up that accounts for each process step: blanking or cutting, deburring, shaping, hole finishing, joining, polishing, and finishing. Allocate a separate budget for plating and enamel or crystal inlays. A typical guideline is to reserve 30–50% of the total tolerance for finishing steps, depending on finish complexity and fixture quality. This planning helps prevent cumulative error in multi-step production and supports scalable private-label runs.
Step 3: Design for finishing compatibility
Design features with plating and enamel in mind. Include generous allowances around recessed areas to accommodate enamel fill and avoid sharp edge overhangs that could trap plating material. When possible, specify uniform edge radii to reduce edge-chipping risk during polishing and handling. Coordinate with OEM and contact teams to confirm capability limits on the chosen finish and to establish test coupons for plating thickness measurement.
Step 4: Establish measurement and quality verification
Develop a standard measurement protocol that includes dimension checks before and after finishing. Use calibrated fixtures to hold parts during measurement, and record plating thickness data alongside dimensional results. Ensure traceability for SGS-compliant audits and supplier qualification. Implement a sample development plan that allows rapid iteration when tolerance drift is observed in new lots.
Step 5: Prototype, test, and iterate
The prototype phase should iterate until the measured tolerances meet target budgets across multiple samples and finishes. Track variance across batches, identify recurring drift, and adjust process windows or fixture designs accordingly. Plan for at least two to three prototype cycles for a robust tolerance validation before mass production. This approach supports private label programs and wholesale partnerships with consistent quality.
Step 6: Documentation and scale-up
Compile a formal tolerance specification package, including mechanical drawings, finishing tolerances, plating thickness ranges, and acceptance criteria. Use this package as the baseline for larger orders and future revisions. Having documented tolerances supports OEM projects and long-term collaborations with distributors and boutique brands, ensuring MOQ adherence and predictable lead times.
Lead time considerations and supply chain alignment
Lead times for tolerance-focused prototyping depend on finish choice and the complexity of the charm. PVD-coated charms may require additional deposition steps, while enamel-filled pieces might need curing and color-shade validation. Plan in advance for measurement setup, fixture fabrication, and finish qualification. For ongoing programs, a structured sample development cycle and pre-approved tolerancing criteria help accelerate bulk orders while maintaining quality. To start a tolerance-driven project, consider engaging with our team through OEM/ODM services and submitting a formal RFQ via Request a Quote.
FAQ
Q1: What tolerance ranges are typical for 316L stainless steel charms?
A typical linear tolerance for small features is ±0.05–0.20 mm, depending on feature size and process. Overall form accuracy depends on the finishing steps and fixture quality. Finishing layers (PVD plating, electroplating, enamel) add thickness in microns, which must be accounted for in the tolerance budget to prevent cumulative drift.
Q2: How does finishing affect tolerances?
PVD plating and electroplating add material thickness that can shift critical dimensions. Enamel fills and crystal inlays also alter depths and surface profiles. Specifying plating thickness targets and enforcing uniform deposition across the charm helps keep dimensional control consistent across lots. working with a 316L stainless steel charms manufacturer that offers precise finishing controls supports reliable results.
Q3: How long does a tolerance-driven prototype typically take?
Prototype cycles usually span 1–2 weeks for initial checks, plus additional time for plating validation and color filling if used. Complex finishes or multi-step processes can extend this to 3–4 weeks. A well-defined sample development plan with pre-approved tolerances reduces iteration cycles and speeds up private-label program readiness.
Q4: How can I start a tolerance-focused prototyping project with Lancy?
Begin by discussing your design, finish, and tolerance targets with our team through our OEM/ODM workflow. Prepare a drawing pack and a finishing specification, then request a formal RFQ via the quote page. We support low MOQ options and scalable private-label packaging for boutique brands and distributors. Learn more about our capabilities at OEM/ODM manufacturing and how we can partner on bulk charm orders with reliable lead times.
Call to action
Partner with Lancy Jewelry for precision-focused 316L stainless steel charms manufacturing. Our modern facility, CNC, laser cutting, laser marking, welding, and polishing capabilities—coupled with SGS-certified processes—enable rigorous tolerance control from prototype to production. If you are evaluating tolerances for a new private-label program or need a reliable supply chain for wholesale stainless steel charms, start an OEM/ODM inquiry or request a formal quote via RFQ / Request a Quote. For questions or technical discussions, contact our team and we will tailor a tolerance strategy and timeline to your project needs.